What Is An Industrial Finned Air Heater And Why Is It Essential In Drying Tunnels?
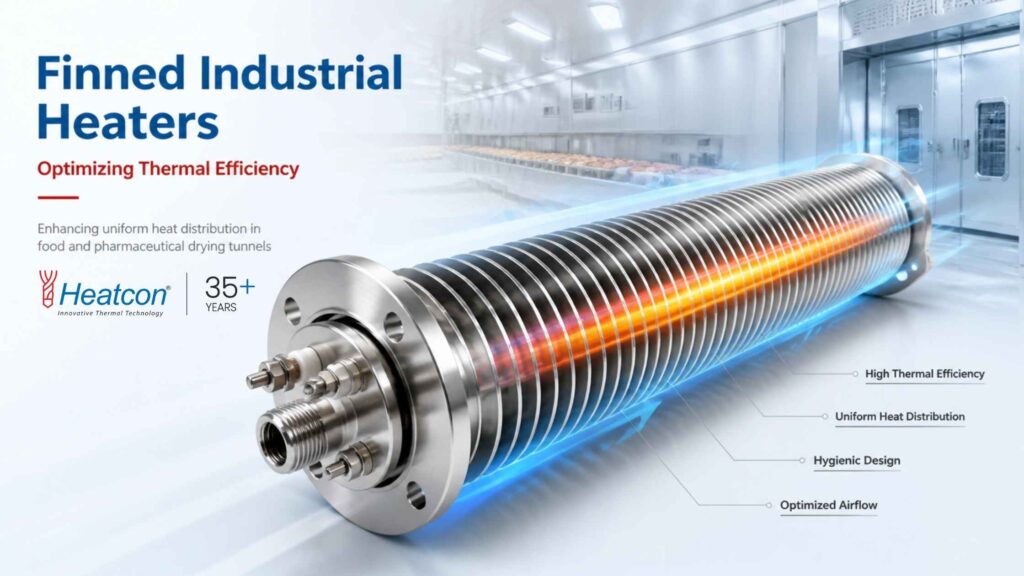
An industrial finned air heater is a specialized electrical heating device designed to deliver uniform hot air across large volumes, making it ideal for continuous drying processes. Its core advantage lies in the presence of fins—metallic extensions that significantly increase the surface area, improving heat transfer rates and ensuring consistent temperature distribution. In food and pharma drying tunnels, the result is faster, more uniform drying, reduced energy wastage, and superior product quality.
- Rapid, uniform drying: Minimizes hotspots and under-dried zones.
- Energy efficiency: Maximizes heat transfer with minimum input power.
- Process control: Works in tandem with precise temperature sensors for optimal results.
The critical role of these heaters in tunnel drying makes them indispensable for manufacturers aiming to meet tight process windows and regulatory standards.
How Do Finned Heating Elements Enhance Energy Efficiency?
Finned heating elements are engineered to optimize the heat exchange between the heater and the air flowing through the tunnel. The addition of fins to the heating tube or cartridge increases the effective area in contact with air, facilitating faster heat transfer. This means a lower surface temperature can achieve the same air temperature rise, reducing both energy consumption and thermal stress on components.
- Greater surface area: Fins multiply the area available for heat exchange.
- Lower operational costs: Less energy is required for the same drying output.
- Longer service life: Lower temperatures mean reduced wear and longer heater lifespan.
In the context of food and pharmaceutical tunnels, this translates to a more controlled, gentle drying process that preserves product integrity and reduces operational costs.
What Are The Key Types Of Industrial Air Heaters Used In Tunnel Drying?
The most effective solutions for tunnel drying processes typically include:
- Finned cartridge heating elements: Compact, high-watt density heaters with fins for superior air heating in limited spaces.
- Process duct air heaters: Designed for integration directly into air ducts, providing powerful, uniform heating for large air flows.
- Industrial air heaters: A broad category including both finned and non-finned variants, with options for custom wattage, voltage, and mounting configurations.
Each type is selected based on application-specific requirements such as air flow rate, tunnel dimensions, temperature range, and product sensitivity.
Why Is Precise Temperature Control Crucial In Food & Pharma Drying?
Precise temperature control is non-negotiable in food and pharmaceutical drying. Too much heat can degrade sensitive ingredients or alter product properties; too little can leave residual moisture, compromising safety and shelf-life.
- Food safety: Ensures pathogens are eliminated without damaging nutrients or texture.
- Pharma compliance: Maintains drug efficacy and meets regulatory requirements.
- Process repeatability: Delivers consistent results across production batches.
This is where Heatcon Sensors’ expertise in custom RTDs and temperature sensors becomes invaluable. By integrating advanced sensors with industrial finned air heater systems, manufacturers can achieve precise, real-time feedback and control, unlocking both efficiency and compliance.
How Heatcon Sensors Delivers Customized Heating And Sensing Solutions Worldwide
Heatcon Sensors is a leading manufacturer of customized RTDs, thermocouples, and other temperature sensors, as well as a diverse range of heat generating equipment. With decades of experience, Heatcon Sensors understands that no two industrial drying tunnels are the same—each demands a tailored approach for optimal results.
- Custom engineered solutions: From finned cartridge heating elements to process duct air heaters, every product is designed to meet your exact process requirements.
- Global supply capability: Heatcon Sensors ships temperature sensors and heating equipment to any location across India, and internationally—including the US, UAE, Indonesia, Germany, South Korea, Saudi Arabia, Russia, Bahrain, Kuwait, and beyond.
- End-to-end support: From design consultation to after-sales service, Heatcon Sensors ensures seamless integration and reliable operation.
In addition to industrial finned air heater solutions, Heatcon Sensors manufactures a complete line of heat generating equipment: industrial furnaces, ovens, hot air blowers, electric furnaces, high density cartridge heaters, and much more. This extensive portfolio means you can source not just heaters, but also the vital sensors and controls, all under one trusted roof.
What Are The Benefits Of Choosing Heatcon Sensors For Your Tunnel Heating Needs?
By partnering with Heatcon Sensors, you unlock a suite of advantages:
- Unmatched customization: Sensors and heaters are tailored to your tunnel’s airflow, temperature, and space constraints.
- Proven reliability: All products are manufactured to stringent quality standards, ensuring safe and uninterrupted operation in critical food and pharma environments.
- Full compliance: Heatcon Sensors’ solutions are designed to help you meet global safety and quality certifications.
- Rapid response: Whether you’re in Mumbai, Riyadh, Jakarta, or Berlin, Heatcon Sensors’ logistics and support network delivers prompt service and technical advice.
Don’t risk production downtime, energy waste, or compliance headaches. Choose the proven partner trusted by leading manufacturers worldwide.
How Can You Reach Heatcon Sensors For Custom Solutions?
Ready to optimize your drying tunnel’s efficiency with advanced heating and sensing solutions? Heatcon Sensors makes it easy to connect and discuss your unique requirements:
- Submit your information on the contact form.
- Leave a message via WhatsApp through the website interface.
- Call for immediate assistance at +91 9164833027 or +91 9844233244.
Act now, and ensure your food or pharmaceutical drying tunnel is equipped for maximum efficiency, quality, and compliance—wherever you operate.
About Heatcon Sensors
Heatcon Sensors is a leading Indian manufacturer and global supplier of industrial heating elements, temperature sensors, and precision process control equipment. With a commitment to innovation, quality, and customer partnership, Heatcon Sensors serves clients in India, the US, UAE, Indonesia, Germany, South Korea, Saudi Arabia, Russia, Bahrain, Kuwait, and worldwide. The company’s extensive portfolio covers customized RTDs, thermocouples, industrial finned air heater solutions, and a complete range of heat generating equipment for critical applications in food, pharma, chemical, and many other industries.
Conclusion: Don’t Settle For Less Than The Best In Tunnel Drying Efficiency
The choice of air heating and temperature sensing technology directly impacts your bottom line in food and pharma tunnel drying. Industrial finned air heater solutions, expertly paired with precise sensors from Heatcon Sensors, ensure that you achieve energy savings, process reliability, and regulatory compliance—no matter where you are in the world. Don’t fall behind competitors who are already reaping the benefits of optimized tunnel heating. Take action today, and take control of your process efficiency with Heatcon Sensors as your trusted partner.