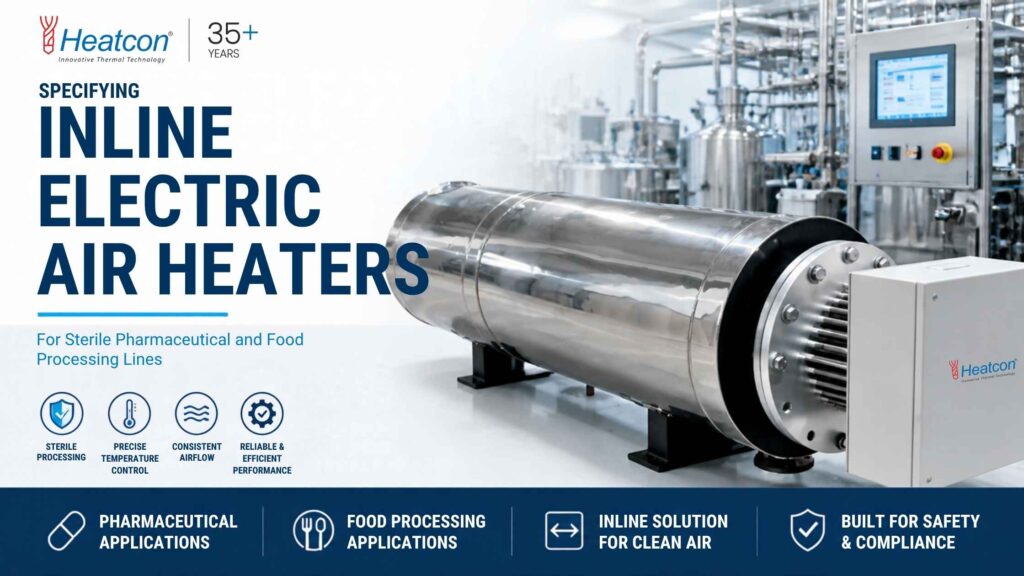
What is the best way to specify an electric inline air heater for sterile pharmaceutical and food processing lines? The most effective approach involves careful evaluation of hygiene, temperature control, airflow, and sensor integration, with a focus on custom solutions tailored to each process and compliance with international standards.
According to industry reports, the global market for electric process heating, including electric inline air heater solutions, is projected to surpass USD 27 billion by 2028, with pharmaceutical and food sectors representing a significant share due to their stringent sterility and process control requirements. In these industries, maintaining precise air temperature and hygiene is not just a matter of efficiency—it’s a matter of safety, quality, and regulatory compliance.
Why is air heating critical in sterile process lines?
Air heating plays a crucial role in sterile pharmaceutical and food processing lines by ensuring product integrity, minimizing microbial contamination, and supporting critical applications such as drying, sterilization, and heat-assisted processing. The choice of an inline electric air heater is pivotal, as it must deliver:
- Consistent, uniform heating to prevent hot or cold spots
- Material compatibility to avoid contamination
- Fast response time for process efficiency
- Simple integration with automation and digital control systems
In sterile environments, any deviation in air temperature or quality can compromise product safety and lead to costly downtimes or recalls.
What are the key considerations for specifying electric inline air heaters?
Specifying an electric inline air heater for sterile environments requires a complete understanding of process requirements and regulatory expectations. The following considerations are essential:
- Hygienic Design: Preference for smooth, crevice-free surfaces (often stainless steel) that are easy to clean and resist corrosion.
- Temperature Accuracy: Precise temperature control is vital. Integration with sensors such as RTDs or thermocouples—customized for the application—ensures tight control and real-time monitoring.
- Airflow and Power: The heater should match the airflow rates and provide enough wattage for rapid heating without overshooting the setpoint.
- Control Systems: A digital controller inline heater enables advanced PID control, programmable setpoints, alarms, and integration with SCADA or PLC systems for data logging and process transparency.
- Compliance and Validation: The heater and its components must comply with FDA, cGMP, and other local/international standards, including validation documentation for IQ/OQ/PQ.
- Maintenance and Serviceability: Design features such as removable elements, easy sensor calibration, and clear diagnostics reduce downtime and ensure reliability.
Types of inline air heating solutions for sterile processes
There are several heater configurations used in pharmaceutical and food processing lines. The most common are:
- Inline electric air heater: Installed directly in the process airflow, providing rapid and precise heating. Suitable for ducted or piped systems, often with integrated sensors for feedback control.
- Cleanroom process heaters: Specifically designed to meet cleanroom standards, featuring minimal particle generation, hermetic sealing, and high-grade materials.
- Process air heater: General term for heaters used in process air streams, including both inline and recirculating types, often custom-sized for the application.
- Digital controller inline heater: Heaters paired with advanced digital controllers offering real-time display, remote monitoring, and programmable logic for precise thermal management.
These solutions can be combined with HEPA filters, UV sterilization, and multi-stage heating for ultra-clean applications.
How does sensor integration improve heater performance?
Sensor integration is the cornerstone of safe, efficient, and compliant heating. Advanced sensors such as Resistance Temperature Detectors (RTDs) and thermocouples are embedded into the heater assembly to deliver:
- Accurate, real-time temperature feedback
- Fail-safes through over-temperature protection
- Remote monitoring and data logging for validation
- Automatic compensation for process variations
Heatcon Sensors specializes in manufacturing custom RTDs and temperature sensors, tailored to each client’s unique process and installation requirements. These sensors are engineered for durability, precision, and hygienic integration—critical for pharmaceutical and food processing lines.
Why choose Heatcon Sensors for custom heating and sensing solutions?
Heatcon Sensors is a leading manufacturer of customized RTDs, thermocouples, and other temperature sensors, as well as heat-generating equipment such as:
- Furnaces (electric, muffle, and tube types)
- Industrial ovens (batch and continuous)
- Hot air blowers and dryers
- Electric inline air heater assemblies
- High density cartridge heaters
- Process air heater solutions for a wide range of industries
- Custom heating mantles and immersion heaters
With a robust manufacturing base and a global logistics network, Heatcon Sensors delivers custom heating and sensing solutions not only across India—including major cities such as Mumbai, Bengaluru, Hyderabad, Chennai, and Delhi—but also worldwide. This includes the United States, UAE, Indonesia, Germany, South Korea, Saudi Arabia, Russia, Bahrain, Kuwait, and beyond.
How to ensure compliance and validation in critical environments?
Compliance with regulatory standards is non-negotiable in pharmaceutical and food processing. Heatcon Sensors ensures all products are manufactured to the highest standards, providing full documentation, calibration certificates, and validation support for:
- cGMP and FDA compliance
- ISO 9001 and ISO 13485 standards
- Documentation for IQ (Installation Qualification), OQ (Operational Qualification), and PQ (Performance Qualification)
Our engineering team assists clients in specifying, installing, and validating heater and sensor assemblies to ensure uninterrupted audits and regulatory approvals.
What are the latest advances in digital heater control?
The integration of a digital controller inline heater has transformed temperature management in sterile process lines. Key advances include:
- PID and fuzzy logic control for ultra-precise temperature stability
- Touchscreen interfaces with remote access and programmable recipes
- Alarm systems for deviation management
- Data logging for traceability and validation
- Seamless integration with plant DCS/SCADA systems
Heatcon Sensors offers digital control solutions that can be tailored to any process, enabling clients to meet the most demanding requirements for quality and repeatability.
How does Heatcon Sensors support customers globally?
Heatcon Sensors is committed to supporting clients in every region. Whether you need an electric inline air heater, custom RTD, or a complete process air heater solution, we offer:
- Custom manufacturing for any specification, volume, or application
- Rapid prototyping and short lead times
- Doorstep delivery across India and international destinations
- 24/7 technical support and application engineering
- Seamless aftersales service and spare parts availability
Our expertise ensures that your process lines remain efficient, compliant, and future-ready—regardless of location.
About Heatcon Sensors
Heatcon Sensors is an ISO-certified manufacturer based in India, specializing in custom temperature sensors, electric heaters, and process control solutions for the pharmaceutical, food, chemical, and manufacturing sectors. With decades of expertise, Heatcon Sensors is trusted by leading companies worldwide for reliable, hygienic, and precise heating solutions. Our products are engineered to meet the toughest standards and are available for immediate dispatch anywhere in India or internationally.
How to contact Heatcon Sensors for your heating and sensing needs?
If you’re looking to specify an electric inline air heater, require custom RTDs or process air heater solutions, or need expert consultation for your sterile process line, Heatcon Sensors is ready to assist. Choose any of the following convenient options:
- Submit your information on our contact form.
- Leave a message on Whatsapp through the interface on our website.
- Call us directly for immediate assistance at +91 9164833027 or +91 9844233244.
Don’t compromise on process integrity, compliance, or efficiency. Partner with Heatcon Sensors—the trusted choice for world-class electric inline air heater and process control solutions.
Frequently Asked Questions
What are the main considerations when specifying an electric inline air heater for sterile processing lines?
Key factors include temperature uniformity, cleanability, material compatibility, and compliance with industry standards. In sterile pharmaceutical and food processing, selecting an electric inline air heater with precise temperature control and hygienic construction is crucial for preventing contamination and ensuring product safety.
How do Heatcon Sensors’ solutions address cleanroom requirements in food and pharma industries?
Heatcon Sensors offers cleanroom process heaters specifically designed for environments with strict hygiene demands. These heaters are built using stainless steel and sanitary fittings, minimizing crevices and particle traps, and they support CIP/SIP protocols to maintain a sterile environment.
Why is a digital controller inline heater beneficial for process control?
A digital controller inline heater enables precise, real-time temperature adjustments and monitoring, which is critical for maintaining consistent process conditions in sterile applications. Heatcon Sensors integrates advanced digital controllers with their heaters to facilitate seamless automation and regulatory compliance.
What materials are used in Heatcon Sensors’ inline electric air heater assemblies?
Heatcon Sensors fabricates its inline electric air heater systems using high-grade stainless steel, PTFE, and other FDA/USDA-compliant materials. This selection ensures both chemical resistance and suitability for sterile processing lines, reducing the risk of product contamination.
Are Heatcon Sensors’ heaters easy to integrate with existing process automation?
Yes, Heatcon’s process air heater solutions are designed for seamless integration with PLCs, SCADA systems, and other plant automation platforms. Their heaters can be supplied with fieldbus communication options and custom control panels to fit specific automation requirements.
How does Heatcon Sensors ensure compliance with industry standards for cleanroom process heaters?
Heatcon Sensors’ cleanroom process heaters are engineered to comply with FDA, cGMP, and ISO requirements. Their documentation includes material traceability, validation support, and certifications as needed for regulated pharmaceutical and food processing environments.
What types of temperature and safety controls can be specified with Heatcon’s inline air heaters?
Heatcon Sensors’ inline air heaters can be configured with integrated PID temperature controllers, over-temperature protection, digital alarms, and remote monitoring capabilities. This ensures both process safety and compliance with validation protocols in sterile lines.
What maintenance and validation support does Heatcon Sensors provide for their process air heaters?
Heatcon Sensors supplies comprehensive documentation, validation protocols, and after-sales support for their process air heater systems. Maintenance is simplified by modular designs and the use of robust, cleanable components, ensuring minimal downtime in critical sterile environments.
Can Heatcon Sensors customize an inline electric air heater to fit unique process requirements?
Absolutely. Heatcon Sensors works closely with clients to design and manufacture inline electric air heater solutions tailored to specific flow rates, temperature ranges, and space constraints, ensuring optimal performance in any sterile pharmaceutical or food processing line.